Deep 45 mm Rib Section Stiffness
The 45/250 profile geometry utilizes 45 mm deep trapezoidal ribs spaced at 250 mm pitch centers to deliver high longitudinal spanning capacity across purlins in large-scale PEB warehouses and industrial workshops.
REGIONAL PROFILES • SAUDI ARABIA & GCC
Technical evaluation and equipment planning guide for steel building fabricators and cladding plants across Riyadh, Dammam, and Jeddah manufacturing 45/250 deep trapezoidal roof and wall sheets. Covers CAD cross-section verification, high-ambient hydraulic cooling considerations, 380V 60Hz three-phase power matching, and containerized shipping to King Abdulaziz Port (Dammam) or Jeddah Islamic Port.
MARKET CONTEXT
Examining structural and environmental factors governing deep-rib trapezoidal sheeting across industrial cities, logistics hubs, and pre-engineered steel buildings (PEB) in Saudi Arabia.
The 45/250 profile geometry utilizes 45 mm deep trapezoidal ribs spaced at 250 mm pitch centers to deliver high longitudinal spanning capacity across purlins in large-scale PEB warehouses and industrial workshops.
Cladding manufacturers in the Gulf region process prepainted aluminum-zinc and galvanized coils engineered for solar reflectance and desert abrasion resistance. Roll tooling surfaces must be finished to protect delicate exterior paint films during deep rib forming.
Accurate side-lap angular nesting and valley pan stiffening flutes help ensure tight longitudinal joint contact on roof and wall envelopes exposed to windborne desert sand and thermal cycling.
MACHINE HIGHLIGHTS
Mechanical design criteria and process considerations evaluated for this profile geometry.
Forming a 45 mm rib depth from standard 1220 mm or 1250 mm input coil requires a multi-station progression that forms center ribs before outer ribs, avoiding strip tearing and minimizing edge wave.
Saudi Arabian industrial zones operate on a 60Hz utility frequency (commonly 380V three-phase). Main drive motors, hydraulic pump motors, and control transformers are wound and calibrated specifically for 380V 60Hz operation.
Hydraulic power packs and electrical control cabinets can be configured with forced-air cooling fans and heat-dissipating enclosures suited to high summer workshop temperatures in Riyadh, Dammam, and Jeddah.
The hydraulic cutoff assembly uses upper and lower shear blades machined to match the 45/250 trapezoidal contour, shearing sheets cleanly without collapsing the 45 mm rib crests.
SPECIFICATION CHECKLIST
Before finalizing machine layout and roll tooling schematics for a Saudi Arabian installation, our engineering team requires confirmation of the following parameters:
TECHNICAL BENCHMARK
Engineering variables and baseline configuration parameters evaluated against customer drawings.
| System Element | Parameter / Specification Baseline | Engineering Review Criterion |
|---|---|---|
| Forming Station Count | Confirmed per signed project contract and 45 mm rib depth simulation | Configured to buyer drawing to distribute bending strain gradually across deep trapezoidal ribs. |
| Roller Tooling Material & Finish | CNC-machined steel rollers with protective hard chrome plating | Polished contact surfaces protect prepainted desert-grade polyester and PVDF coil coatings. |
| Main Shaft & Stand Construction | Solid machined steel shafts mounted in rigid stand housings | Sized per signed project contract to prevent shaft deflection across thick commercial gauges. |
| Hydraulic Cutoff Unit | Post-cut hydraulic profile shear configured to buyer drawing | Contoured shear blades match upper and lower sheet ribs for clean transverse cuts. |
| Electrical & PLC Control System | 380V 60Hz 3-phase industrial package with bilingual HMI options | Includes rotary encoder length measurement, batch counting, and thermal overload protection. |
WORKSHOP VIEWS / PROJECT DISCUSSION
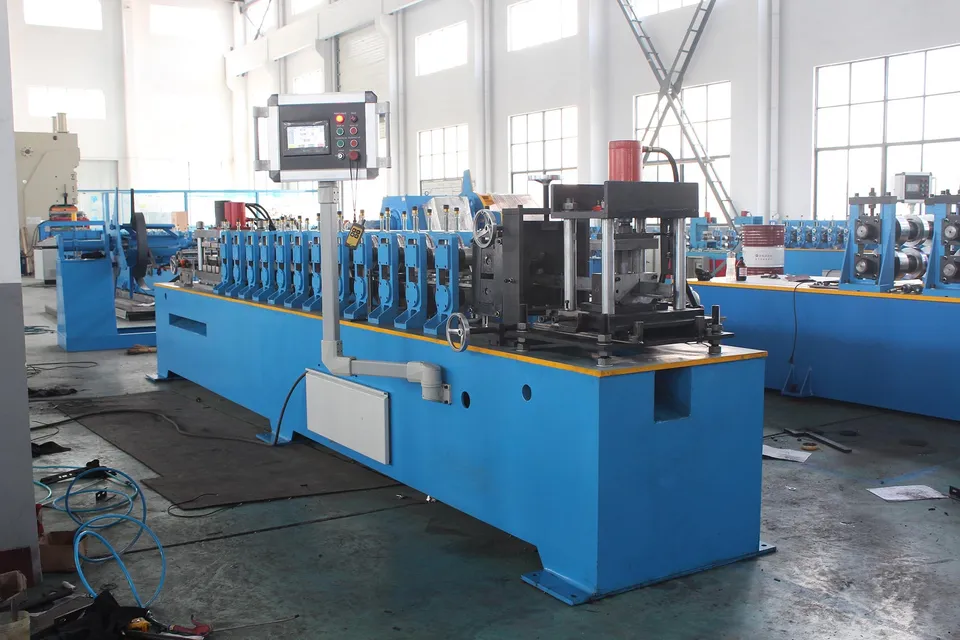
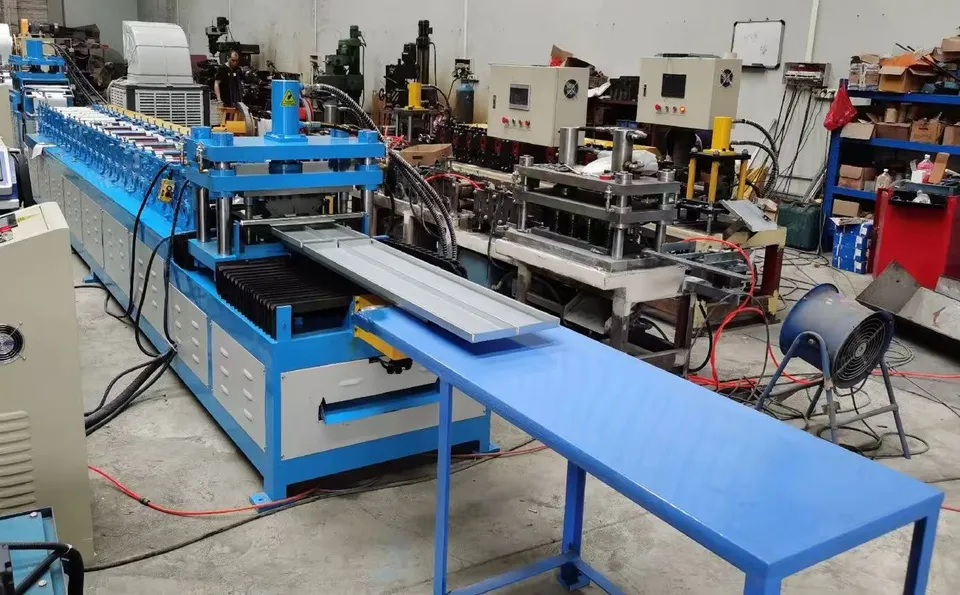
Workshop-zone views of multi-station roll forming lines and profile cutoff assemblies. Captions describe visible mechanical arrangements. They do not certify specific output or individual plant performance.
TECHNICAL FAQ
Technical clarifications on tooling design inputs, operating limits, and production feasibility.
Yes, provided the decimal thickness range and minimum bend radii are confirmed during engineering review. Processing aluminum alongside prepainted steel requires smooth roller finishes and verified roll gap clearances.
Unlike 50Hz machinery that would run at incorrect speeds or overheat on a 60Hz grid, we specify motors, gear reducers, hydraulic pumps, and VFD parameters wound and rated directly for 380V 60Hz three-phase industrial supply.
Each profile family uses dedicated forming stands, but PEB fabricators frequently pair a 45/250 roof/wall cladding line with a separate C/Z structural purlin roll forming line to supply complete building envelope packages.
Machinery is modularly packed, treated with anti-corrosion oil, and braced inside 40ft containers for shipment from Tianjin Port to King Abdulaziz Port in Dammam (for Eastern Province and Riyadh) or Jeddah Islamic Port.
Send your 45/250 or custom trapezoidal CAD drawing, coil thickness range, and 380V 60Hz workshop details. Our engineering desk will prepare a project-specific equipment proposal.
Reviewing deep-rib warehouse cladding and solar mounting strut lines for UAE industrial zones?
Review alternative profile specifications →FACT VERIFICATION
External industry references documenting regional profile nomenclature and commercial sheet sections.
Regional Profile Reference: Trapezoidal 45/250 Roofing & Cladding (Rigidal / GCC) ↗
Regional manufacturer overview illustrating typical 45/250 trapezoidal rib geometry used across Middle East industrial projects.
Saudi Industrial Electrical Frequency & Voltage Context (SEC) ↗
Utility reference for 60Hz grid operation across industrial sectors in the Kingdom of Saudi Arabia.