Include the surrounding equipment
- Surface-conscious roll tooling and lubrication
- Dense-array punching
- Straightening after asymmetric punching
- Cutoff, marking and packing
TAIBANG / EQUIPMENT
Solar PV mounting strut channel (41x41 / 41x21 mm) and tracker bracket roll forming lines for 1.2-3.5 mm GI and ZAM coated steel. Vacuum-hardened DC53 dense slot punching & surface-safe rolls.
APPLICATION & EQUIPMENT
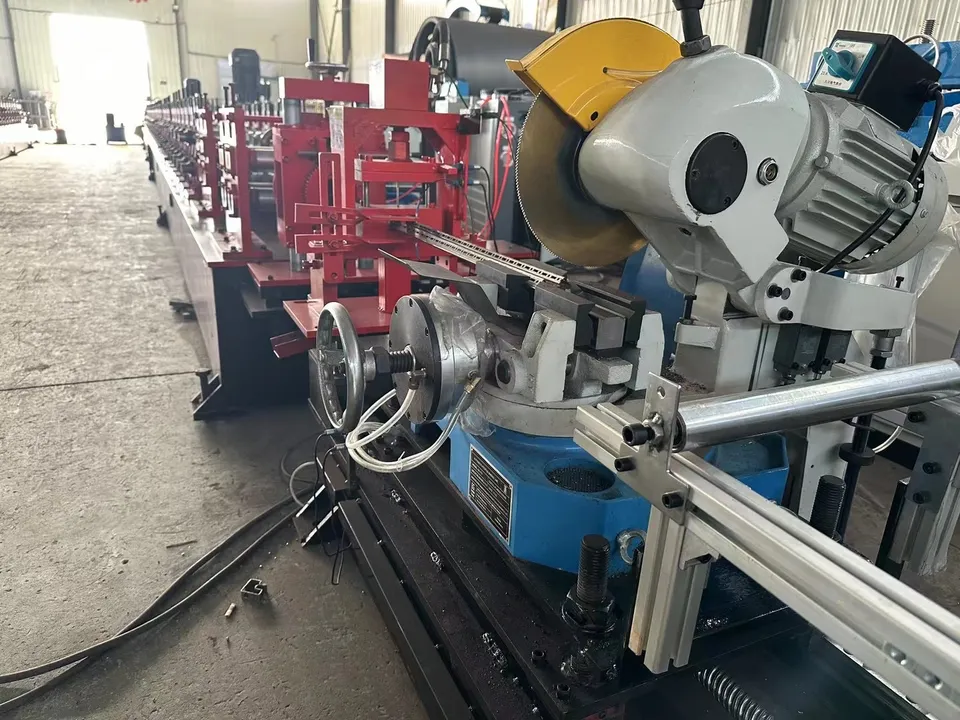
Solar mounting equipment is specified from the finished channel or bracket: strut width, return geometry, thickness, coating system and the hole or slot array used for module clamps and tracker hardware. Zinc-aluminum-magnesium and other coated coils need an agreed surface-inspection method because roll contact can mark the coating. Reviewed workshop photographs of infeed rollers and forming housings are general shop views. They are not photographs of a named solar-strut model and do not show a solar farm.
YOUR SPECIFICATION BRIEF
Share the details you have. If a dimension or requirement is undecided, describe the intended finished product.
| Project item | What to include |
|---|---|
| Profile drawing | Strut or bracket section, returns, internal clearance and cut lengths. |
| Coil and coating | Grade, yield discussion range, coating system and any anti-scratch handling requirements. |
| Hole array | Clamp slots, adjustment holes, pitch, cumulative tolerance discussion and marking needs. |
| Product mix | Channel lengths, bracket variants and whether several sections share tooling. |
| Workshop | Coil handling, surface protection, punching scrap and packing method. |
Speed, power, tooling, tolerances and control components belong in the agreed machine specification. They are not fixed across this equipment category.
ENGINEERING REFERENCE PARAMETERS
The following engineering baseline reflects measured workshop machine parameters and tooling standards. These figures are category references, not a fixed machine specification.
| Engineering Subsystem | Design Range & Workshop Baseline |
|---|---|
| Section Discussion Range | Open strut channels, hat or C-style mounting profiles, and tracker brackets when the same project lists them. Geometry is taken from the drawing; this page does not publish a module-brand mounting standard. |
| Material & Coating Baseline | Engineering discussion range commonly includes structural coated coil around 1.2 to 3.5 mm, including hot-dip galvanized or zinc-aluminum-magnesium finishes named by the buyer. Exact coating mass and surface-acceptance photos are confirmed per signed project. |
| Punching & Marking Baseline | Mounting slots and holes may be punched in a dense array. In-line marking, if required, is an optional station. Cumulative pitch over long channels is a measurement-method discussion, not a published catalog tolerance. |
| Tooling & Surface Handling | Roll material, chrome or lubrication choices are discussed to reduce coating marks. They are process options, not a promise of unmarked coil. Straightening may be required after asymmetric punching. |
| Line Speed Discussion Range | Forming discussion often sits around 8 to 18 meters per minute before dense punching and packing are included. Usable output follows the hole array, cut length and handling rules agreed for the project. |
| Electrical & Destination Requirements | Drive motors carry CE attestation (Certificate M.2023.206.C82549) under EU Machinery Directive 2006/42/EC and EMC Directive 2014/30/EU, verified by UDEM International through March 2028. Voltage, language and guarding are matched in the offer. |
SPECIFICATION BOUNDARY
Specifications on this page are either verified brochure baselines or engineering discussion ranges. Final line layout, drive sizing, roll-stand count, tooling material, tolerances and acceptance criteria are confirmed in your signed project offer — they are not fixed by this page. Workshop photos and video show general shop arrangements and mechanical motion; they are not images of a named, quoted machine model.
* Engineering discussion range / workshop baseline; confirmed per signed project. Photographs and video are reviewed workshop assets reused as process views, not images of this exact solar-strut line.
FROM BRIEF TO ACCEPTANCE
Confirm strut or bracket geometry
Review coating and handling rules
Map the hole array and marking
Agree forming, straightening and cutoff
Inspect coating and pitch on trial lengths
WORKSHOP VIEWS / PROJECT DISCUSSION
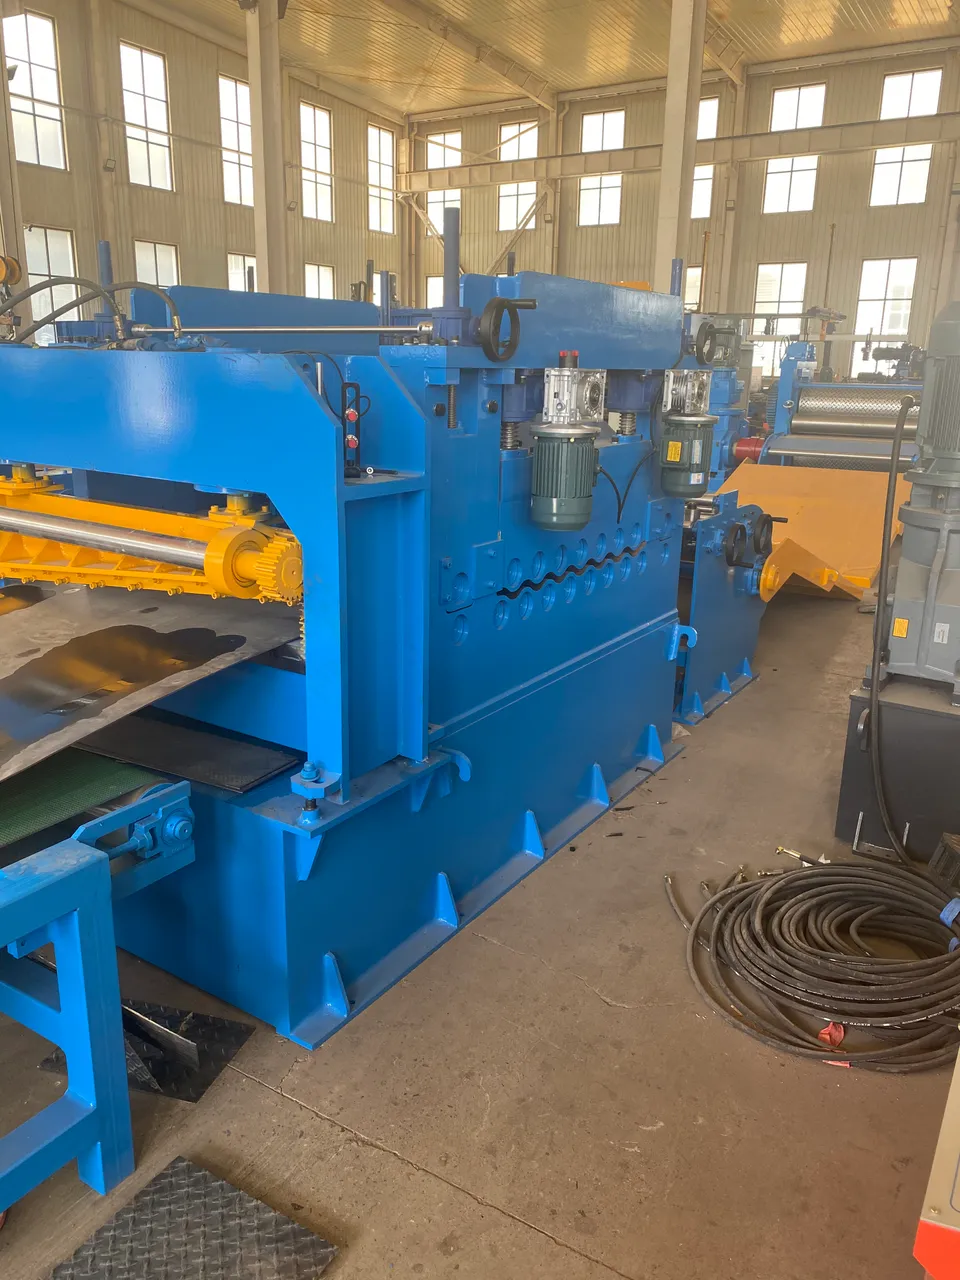
Supplied workshop photos are reviewed shop views of infeed rollers and forming housings in the workshop. They are not photographs of a named PV strut model and do not show a solar farm. Confirm coating handling, hole array and trial inspection in the project offer.
WORKSHOP VERIFICATION / ROLL TOOLING
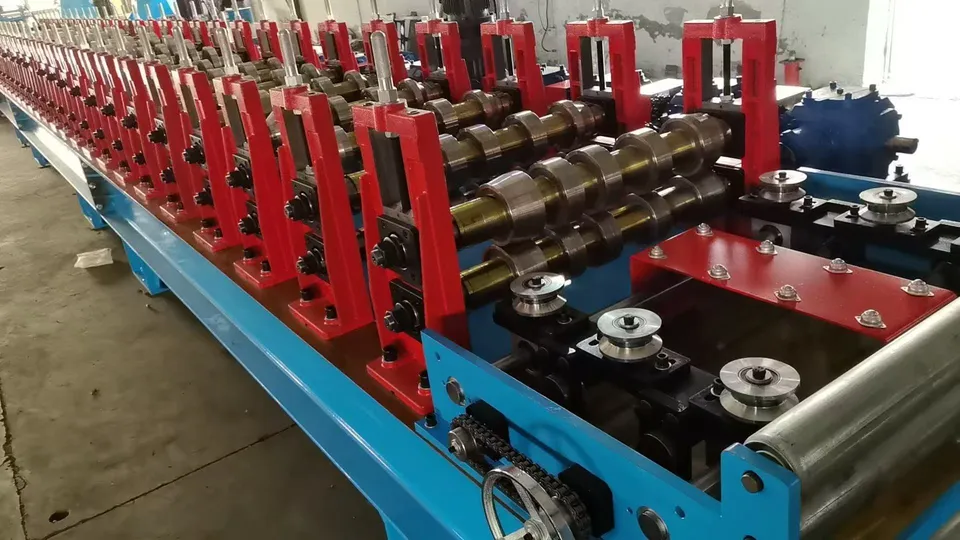
Reviewed close-up footage of roller tooling in the workshop. It shows roll contact and stand hardware, not a named PV strut model or a coating-performance result.
Silent workshop footage; it shows mechanical motion, not a quoted machine's output.
Plan your machine inspection ↗Record trial material, sample measurements, the operating cycle and the documents needed for acceptance.
Inspection planning ↗SOLAR STRUT BUYER BRIEF
| Decision area | What to define before quote comparison |
|---|---|
| Profile family | Strut channel, C-style mounting channel, U-style channel or Z bracket. Treat these as related ranges, not as one guaranteed tooling set. |
| Punching density | Slot shape, hole pitch, edge margin, cumulative pitch measurement and slug removal. Dense punching is often the reliability bottleneck. |
| Coil yield and coating | Yield-strength range, thickness band, galvanized or zinc-aluminum-magnesium coating, strip width and surface-inspection method. |
| FAT evidence | Trial coil or approved substitute, measured hole pitch, coating-mark review, straightness, cutoff length and punch-list closure before packing. |
This page does not publish a universal list price or a fixed warranty period. Solar mounting projects are quoted from drawings, coil inputs, punching scope and factory-acceptance evidence.
RELATED EQUIPMENT
These families are often specified together. Open a related line to compare the equipment scope.
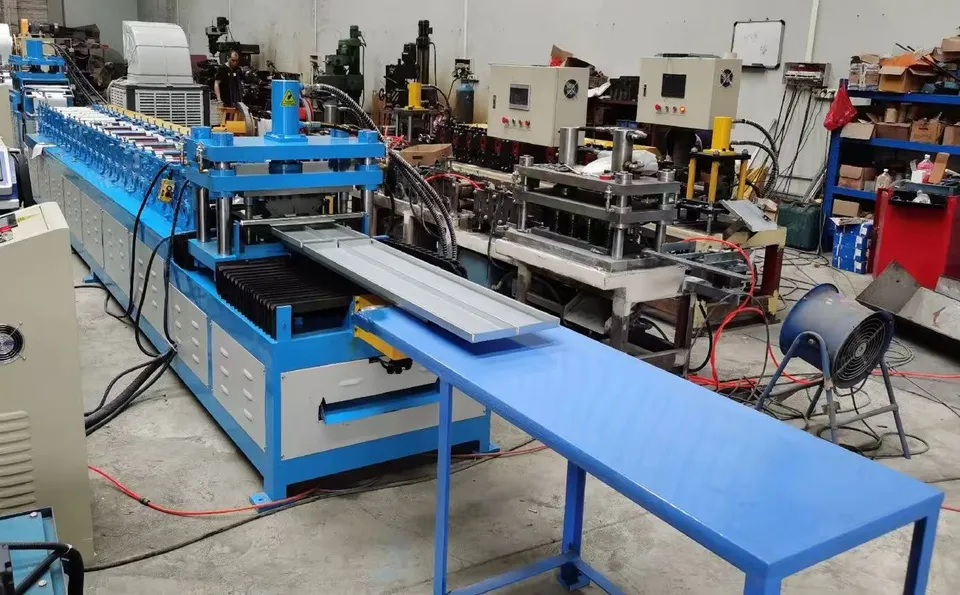
Light-gauge steel C-stud and U-track roll forming machines for 0.4-1.5 mm galvanized strip (50-150 mm web widths). In-line service hole punching, dimpling, flying shear & motorized width sizing.
Explore equipment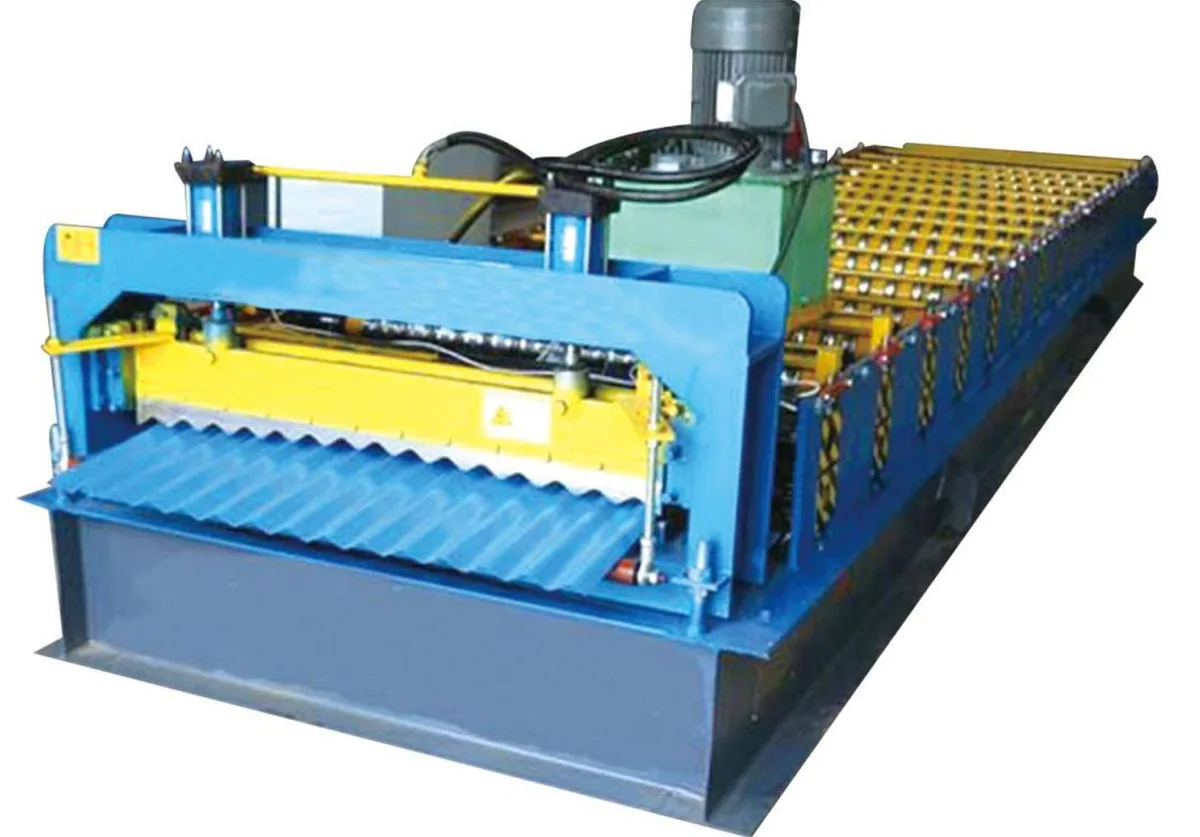
Custom metal roofing and wall cladding roll forming machines for 0.3-0.8 mm PPGI, GI and Aluzinc coil. Solid 70-75 mm shafts, Cr12 hydraulic shear, 380V-480V grid match & workshop trial video.
Explore equipmentBEFORE YOU REQUEST A QUOTE
Continuous PV strut lines require dense mounting slots that create high die wear and slug accumulation. We use vacuum-hardened DC53 punch dies with pressurized air ejection and reinforced slug chutes, preventing die jamming and ensuring stable multi-shift punch life.
Yes, our solar strut lines feature adjustable forming stands or quick-change cassette roll units that switch between standard 41x41 mm deep strut and 41x21 mm shallow channel in 20 to 30 minutes without needing to disassemble the main drive transmission shafts.
Our tooling is crafted with Cr12MoV vacuum-quenched steel and specialized micro-polished PVD surface finishing. Combined with controlled water-soluble emulsion misting, it eliminates zinc galling and preserves the protective self-healing layer on ZAM steel coils.
The machine body is protected with anti-rust oil, wrapped in waterproof film and shock-absorbent foam, and securely braced inside 20GP or 40HQ containers. Sensitive PLC control cabinets and hydraulic pump stations are packed in seaworthy wooden crates.
Typical fabrication lead time commonly ranges from 30 to 60 working days after receipt of the deposit and formal sign-off on tooling profile drawings. Multi-profile configurations or custom electrical specifications are scheduled per project agreement.
We provide technical assistance including remote video troubleshooting, rapid express delivery of spare parts, and on-site engineer dispatch for commissioning or repairs where agreed in the project contract.
Each line ships with a standard wearable parts kit including limit switches, relay fuses, hydraulic seals, and adjusting tools. Custom spare packages including profile shear blades and punch die inserts are quoted per project requirements.
Yes, all drive motors and electrical cabinets are customized to match your local industrial grid, such as 380V, 415V, 440V, or 220V 3-phase at 50Hz or 60Hz. We configure industrial electrical components from recognized suppliers with proper thermal overloads to ensure stable operation.
We provide comprehensive step-by-step video manuals and remote video technical support for machine setup and trial runs. On-site engineer dispatch for commissioning and operator training is available upon request and confirmed in the sales agreement.
Our minimum order quantity is 1 set. Whether you are starting a new fabrication workshop or adding a specialized line to an existing plant, we design, test, and ship complete custom roll forming lines with full technical documentation for single-machine orders.
We accept T/T with a 30% advance deposit upon contract signing and 70% balance payment after factory trial acceptance and prior to sea shipment. Irrevocable letters of credit (L/C at sight) are also accepted upon mutual financial agreement.
DIRECT INQUIRY
Start your project brief
Your name, email and project requirements are enough to start. Required fields are marked *. Our engineering desk targets a reply within 12 hours (China time, UTC+8) — a communication target, not a contractual SLA.
Your next production line
Send your drawing, material, finished output target and destination. Build the equipment, inspection and delivery scope into one project brief.