Include the surrounding equipment
- Decoiling and leveling
- Universal adjustable forming stands
- In-line slot punching or pre-punching
- Cutoff and piece counting
TAIBANG / EQUIPMENT
Form door frame guide rails and universal square channels. One machine produces multiple sizes through quick changeover.
APPLICATION & EQUIPMENT
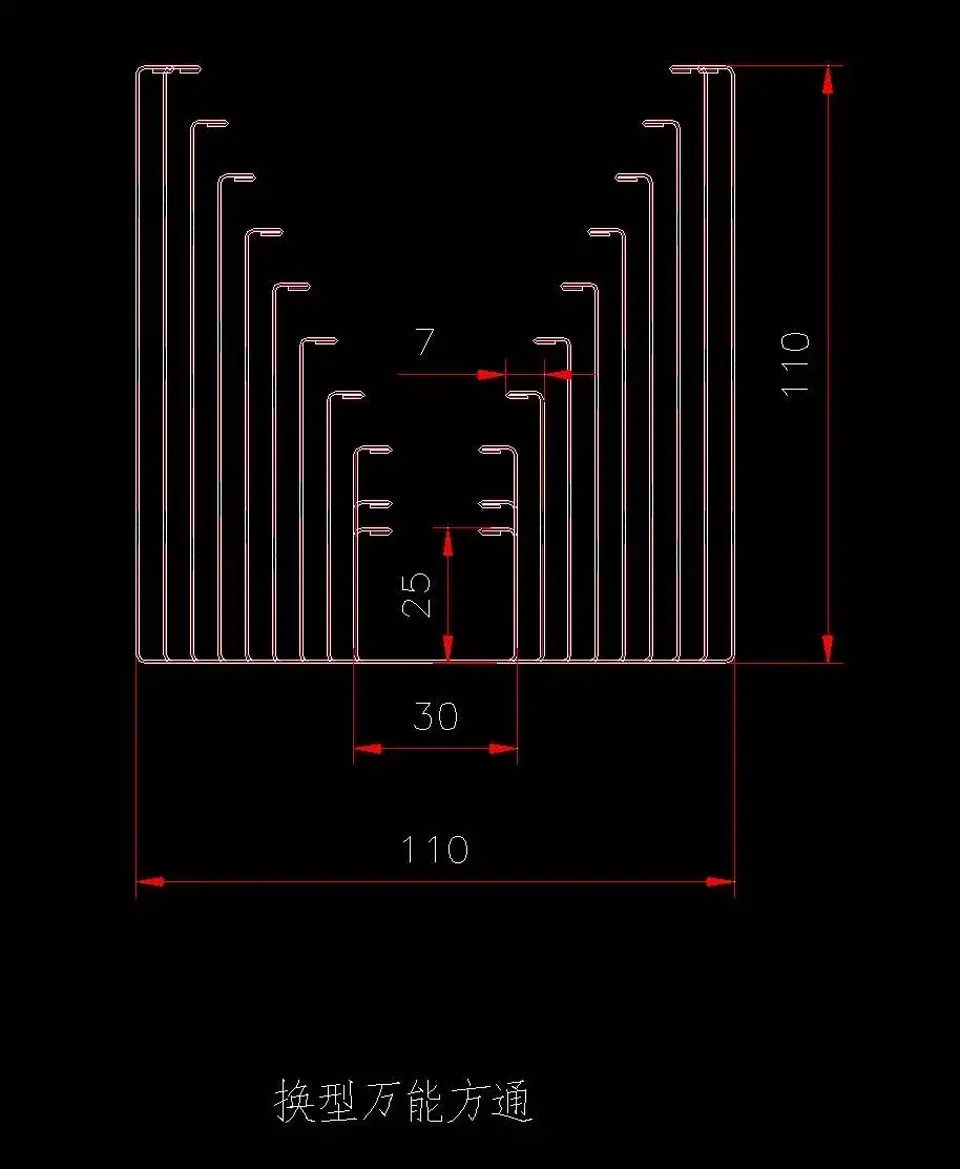
Door frame guide rail equipment produces square or rectangular channel profiles used in door frames, window frames, partition tracks and industrial racking. The key feature is "universal channel" capability: one set of tooling produces multiple section sizes (e.g. 110×110 mm with internal slot variations) through adjustable forming stands. The profile often includes an internal slot (30×25 mm shown in the standard drawing) for guide rail function. Specify the outer section dimensions, internal slot geometry, material and the size family that must share the same tooling.
YOUR SPECIFICATION BRIEF
Share the details you have. If a dimension or requirement is undecided, describe the intended finished product.
| Project item | What to include |
|---|---|
| Section geometry | Outer dimensions (e.g. 110×110 mm), internal slot size and position, wall thickness. |
| Size family | All section sizes that must share the same forming tooling; changeover range. |
| Material specification | Grade, coating, thickness range and coil width. |
| Internal slot requirements | Slot dimensions (e.g. 30×25 mm), position tolerance and function. |
| Production target | Pieces per shift, length mix and size changeover frequency. |
Speed, power, tooling, tolerances and control components belong in the agreed machine specification. They are not fixed across this equipment category.
ENGINEERING REFERENCE PARAMETERS
The following engineering baseline reflects measured workshop machine parameters and tooling standards. These figures are category references, not a fixed machine specification.
| Engineering Subsystem | Design Range & Workshop Baseline |
|---|---|
| Profile Family | Universal square channel sections for door frame guide rails. Standard reference section: 110×110 mm outer with 30×25 mm internal guide slot. Multiple sizes from a single adjustable tooling set through quick changeover. |
| Material & Thickness Baseline | Galvanized or cold-rolled steel coil. Thickness discussion range: 0.8 to 2.0 mm. Coil width matched to section perimeter plus forming allowance. |
| Forming & Changeover | Multi-position adjustable forming stands ("换型万能方通" universal changeover design). Stand count typically 10 to 16. Quick-change mechanism allows different section sizes without full roll replacement. |
| Slot & Cutoff Specifications | Internal guide slot formed or punched in line. Slot dimension tolerance discussion: within 0.5 mm. Flying or stop-cut shear for finished length; cut length accuracy reference: within 1.0 mm. |
| Line Speed Discussion Range | Continuous forming speed discussion: 12 to 25 meters per minute for standard wall thickness. Size changeover time: 15 to 30 minutes for manual-adjust tooling. |
| Electrical & Destination Standards | Drive motors carry CE attestation (Certificate M.2023.206.C82549) under EU Machinery Directive 2006/42/EC and EMC Directive 2014/30/EU, verified by UDEM International through March 2028. PLC control with touchscreen HMI; voltage and guarding adapted per project. |
SPECIFICATION BOUNDARY
Specifications on this page are either verified brochure baselines or engineering discussion ranges. Final line layout, drive sizing, roll-stand count, tooling material, tolerances and acceptance criteria are confirmed in your signed project offer — they are not fixed by this page. Workshop photos and video show general shop arrangements and mechanical motion; they are not images of a named, quoted machine model.
* Engineering discussion range / workshop baseline; confirmed per signed project. Profile drawing is a factory-supplied CAD section showing the universal changeover concept.
FROM BRIEF TO ACCEPTANCE
Confirm section dimensions and internal slot
Review material and thickness range
Plan multi-size changeover method
Agree cutoff and length tolerance
Inspect trial pieces for section and slot accuracy
WORKSHOP VIEWS / PROJECT DISCUSSION
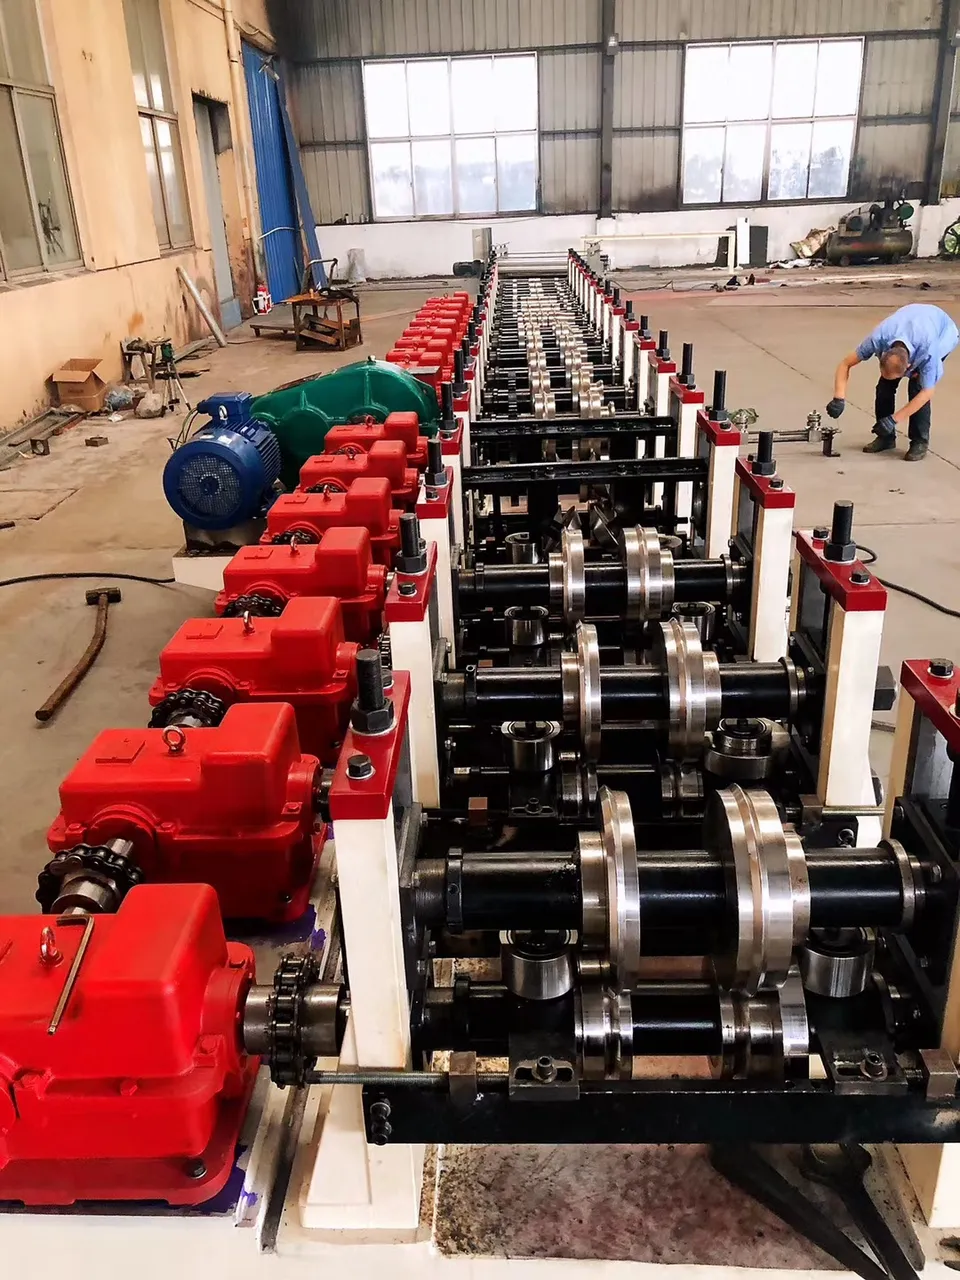
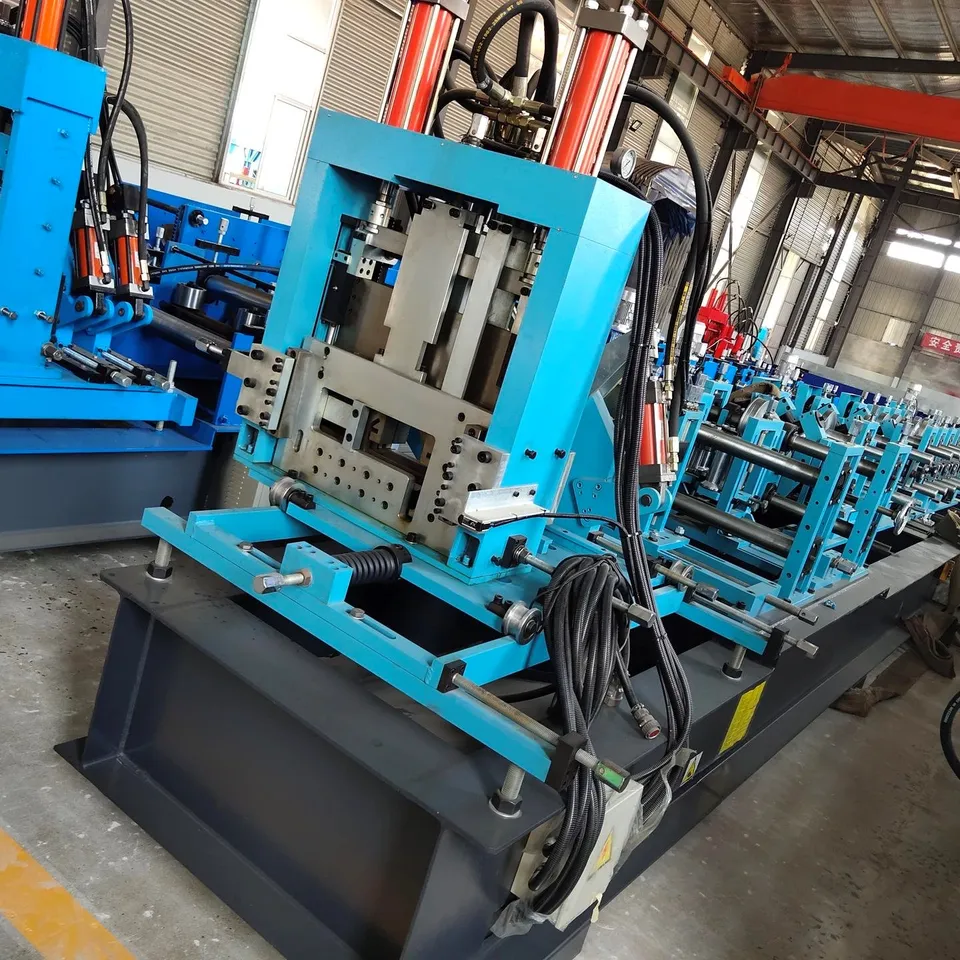
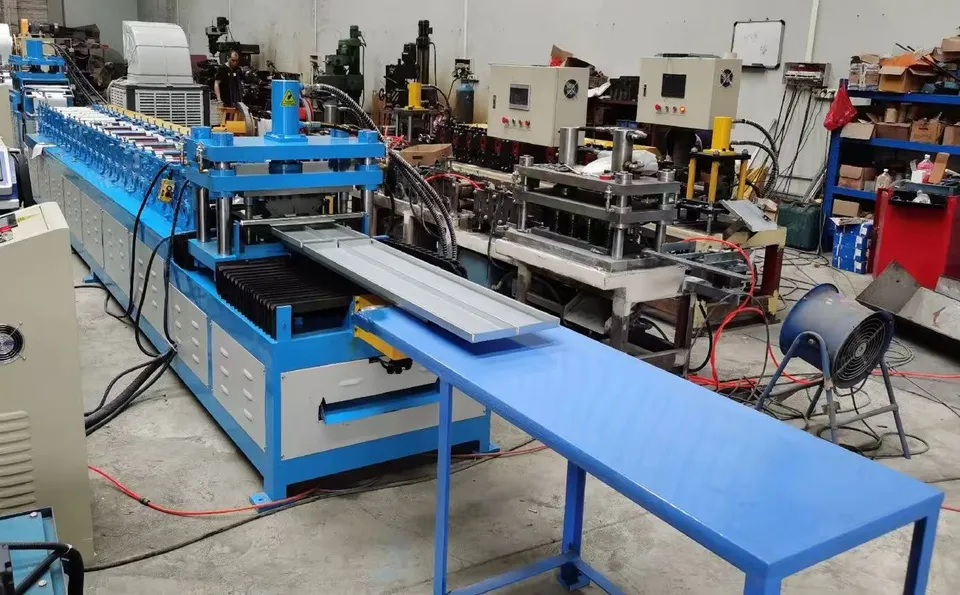
Supplied workshop photos are reviewed shop views of forming equipment and press stations. They illustrate general shop arrangements, not a named door frame guide rail model. Confirm section dimensions, slot geometry and changeover range in the project offer.
WORKSHOP VERIFICATION / GUIDE RAIL FORMING
Workshop footage of forming and pressing stations for door frame guide rail production.
Silent workshop footage; it shows mechanical motion, not a quoted machine's output.
Plan your machine inspection ↗Record trial material, sample measurements, the operating cycle and the documents needed for acceptance.
Inspection planning ↗RELATED EQUIPMENT
These families are often specified together. Open a related line to compare the equipment scope.
Form light-gauge studs, tracks and related interior channels. Start with the section, thickness and in-line holes.
Explore equipment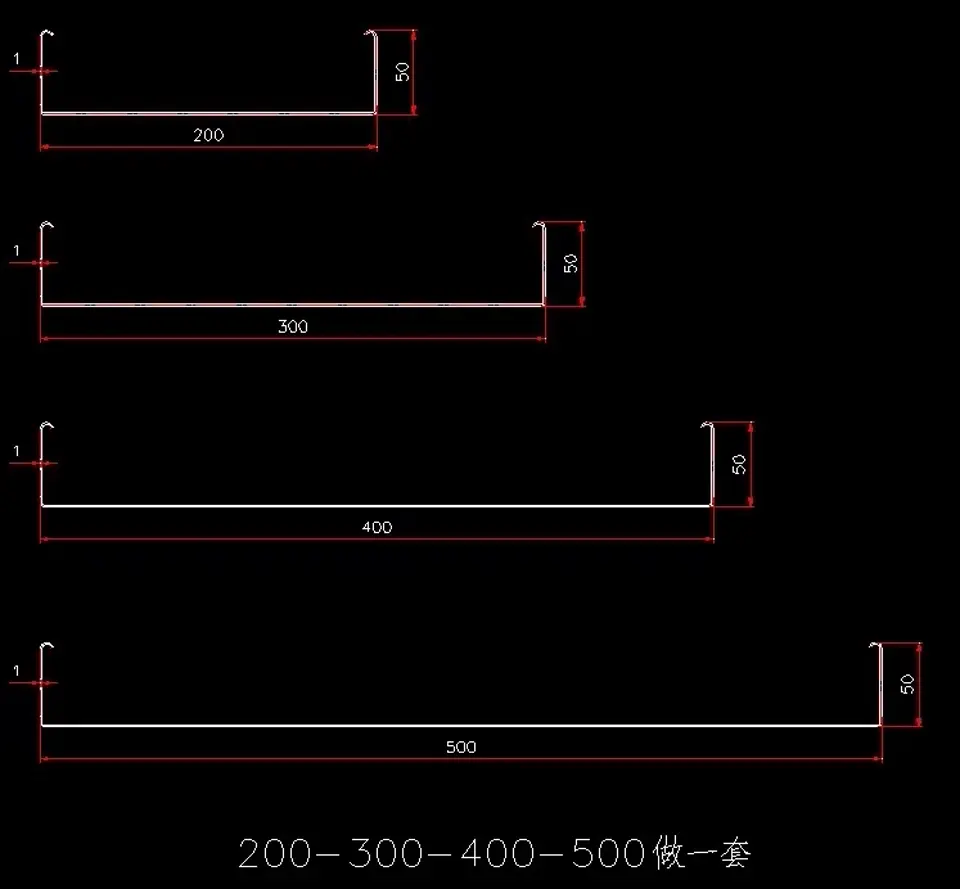
Form U-channel cargo box panels in multiple widths from a single set of tooling. Define the channel width range, flange height and material.
Explore equipmentBEFORE YOU REQUEST A QUOTE
Yes. Describe your intended panel or sheet in text. Contact info@tbrollforming.com to discuss sharing a sketch or reference image; this form does not upload files. Final tooling and pricing need an agreed technical brief.
Discuss the material, product geometry, length mix and full operating cycle. Forming speed alone does not describe finished output per shift.
Ask for a written offer that defines the equipment list, optional items, inspection, delivery terms, installation responsibilities and support scope.
Your next production line
Send your drawing, material, finished output target and destination. Build the equipment, inspection and delivery scope into one project brief.